Ultrasonic Homogenizer for High-temperature Oil Treatment
Views: 60 Author: Site Editor Publish Time: 2026-10-28 Origin: Site
Ultrasonic Homogenizer for High-temperature Oil Treatment
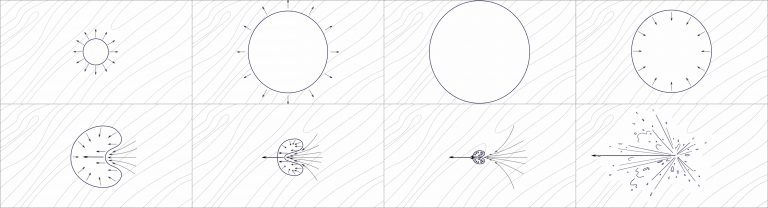
Ultrasonic sonotrodes (or probes) are used in high-temperature oil bath processing. Their primary advantage lies in the ultrasonic cavitation effect, which enhances mass transfer, promotes mixing and dispersion, and can accelerate certain physical or chemical processes. However, the specific outcome depends on factors such as the type of oil, its temperature and viscosity, and whether the ultrasound is applied directly to the oil or used to heat the material indirectly via the oil bath.
I. Key Advantages of Ultrasonic Probes in High-Temperature Oil Baths
1. Enhanced Mixing and Mass Transfer
Micro-jets, localized shear forces, and acoustic streaming—generated by ultrasonic cavitation—facilitate the mixing of various components within an oil medium and improve mass transfer efficiency in certain systems. This can help achieve more uniform dispersion of solid particles, additives, or other components that are otherwise difficult to disperse in an oil phase.
2. Promotion of Emulsification and Droplet Refinement
When an aqueous phase or another immiscible liquid is present in the oil, ultrasound helps break down droplets and reduce their size, resulting in a finer emulsion. However, the stability of the emulsion remains dependent on the formulation, the emulsifiers used, and subsequent processing conditions.
3. Enhanced Extraction and Dissolution in the Oil Phase
For plant-based raw materials, solid additives, or substances containing soluble components, ultrasonic cavitation and localized shear can improve solid-liquid contact, thereby promoting the transfer of target components into the oil phase. The actual increase in extraction yield must be verified through experimentation.
4. Intensification of High-Temperature Processes
For systems suitable for ultrasonic treatment, ultrasound can be combined with heating; the synergistic effect of temperature and cavitation can enhance processing efficiency. It should be noted, however, that ultrasound itself generates heat, and it does not necessarily shorten processing times for all types of applications.
II. How Does This Differ from a Conventional High-Temperature Oil Bath?
Comparison Items
Simple high-temperature oil bath
High-temperature oil bath + ultrasonic probe
main function
Promote reactions, dissolution or softening through heat.
Combination of thermal effect and ultrasonic mechanical effect
Mixing and dispersion
Depend on natural convection or mechanical stirring
Can enhance local shear and dispersion
Solid-liquid mass transfer
Mainly relying on temperature and contact area
May further promote solid-liquid mass transfer
emulsifying effect
Simple heating usually cannot effectively refine the droplets.
Under appropriate conditions, the droplets can be refined.
Reduce viscosity
It is usually a temporary decrease caused by the increase in temperature.
It may cause either rheological changes or compositional variations simultaneously, and the effect will depend on the type of oil.
temperature control
Controlled by an oil bath heating system
Both the heat generated by heating and that produced by ultrasound need to be taken into consideration simultaneously.
In research on heavy oils or residual oils, ultrasonic treatment has been shown to reduce viscosity; however, these findings cannot be directly applied to all industrial oil products.
III. Three Key Considerations for High-Temperature Applications
1. Temperature Resistance of the Ultrasonic Probe
Standard laboratory ultrasonic probes are not necessarily suitable for high-temperature oil baths. It is essential to verify the continuous operating temperature limits for the transducer, horn (booster), probe tip, sealing components, and cooling system. If the oil temperature reaches 100°C, 150°C, or higher, the system must be specifically designed for the actual operating conditions; one cannot rely solely on the temperature resistance of the titanium alloy probe tip.
2. Higher Temperatures Do Not Always Enhance Cavitation
Rising temperatures alter the viscosity, vapor pressure, and dissolved gas content of the oil; therefore, cavitation intensity does not necessarily increase with temperature. Optimal conditions should be determined through comparative experiments involving various temperatures, amplitudes, and processing durations.
3. Oil Oxidation and Safety
Ultrasonic processing can cause localized heating, oxidation, or other chemical changes in the oil. When dealing with flammable oils, it is critical to evaluate factors such as flash point, volatility, pressure within a closed system, and explosion-proof requirements. Furthermore, the probe must never be operated without a load (i.e., while not submerged in the medium) or allowed to collide with the walls of the container.
While ultrasonic probes offer significant potential, for industrial lubricating oils at temperatures exceeding 200°C, it is recommended to adopt an approach that combines a specialized high-temperature ultrasonic probe with a temperature-controlled reaction vessel, supported by small-scale comparative testing. Simply inserting a standard ultrasonic probe into hot oil for long-term operation is not advisable.